
How to Choose Chemical Resistant Flooring: Food-Grade, Anti-Static and Screed Systems
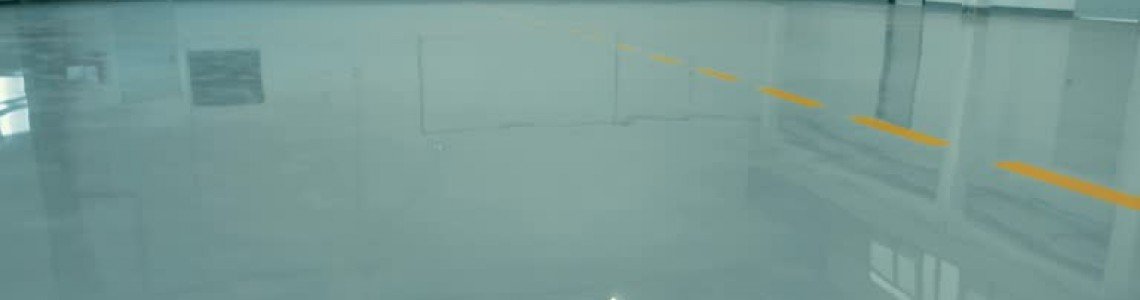
Plants rarely replace a floor because it looks old. They replaced it because something failed. An acid spill lifted the coating, a forklift chipped the edge, or an auditor found cracks where water and bacteria sit. Choosing chemical resistant flooring before that happens costs far less than a forced shutdown. This guide explains how to match a system to your process, what to check before placing an order, and where projects usually go wrong.
What Chemical Resistant Flooring Really Means

Chemical resistant flooring is a floor system that keeps its strength, bond and surface when acids, alkalis, solvents, oils or cleaning agents land on it. No floor resists everything. A coating that handles dilute acid well can soften under a strong solvent. So the first job is not picking a product. It is listing what actually touches the floor.
Collect these details before you talk to any supplier:
Chemicals and their concentrations
Temperature of spills and wash water
How long a spill usually sits before cleanup
Type of traffic: foot, pallet jacks, forklifts, steel wheels
Cleaning method: mopping, scrubbing, steam or pressure wash
With this list, a good supplier can narrow your options in one conversation.
Common Types of Chemical Resistant Flooring at a Glance
Treat these chemical resistant flooring options as starting ranges. Actual thickness depends on the load and the concrete below.
Choosing Chemical Resistant Flooring by Industry

Pharma and labs: A seamless surface that is easy to clean matters most. Smooth epoxy with coved skirting at the wall keeps dust and microbes out of corners. Here, chemical resistant flooring must also handle disinfectants, which are often harsher than the process chemicals.
Electronics and cleanrooms: Static discharge is the risk. Anti-static systems use conductive fillers and an earthing grid. Resistance values should be tested after installation, not assumed from the data sheet.
Food and beverage: Hot water, fats, sugar and organic acids are the usual problems. Wet processing areas often need a PU screed because it copes with temperature swings during steam cleaning. For dry areas, food safe epoxy is common. Ask for low-odor, non-tainting grades, and ask for test reports your auditor will accept.
Chemical plants and battery rooms: Strong acids call for novolac epoxy or vinyl ester systems, along with bunded areas for containment.
Automotive and engineering: Oils, coolants, brake fluid and heavy wheels. A thick epoxy mortar or industrial epoxy resin flooring with a hard-wearing topcoat usually performs better than a thin coat.
Where Industrial Screed Flooring Fits
Industrial screed flooring is a thicker, trowel-applied layer, usually 5 mm or more, made from resin mixed with graded aggregates. It suits places where a thin coat would fail: heavy impact, hot spills, steam cleaning, or daily forklift traffic. It also hides small surface flaws in the concrete better than a thin coat does.
The trade-off is cost and skill. Screeds need correct mixing, even thickness and clean joint detailing. A badly laid screed can fail sooner than a well-done thin coat, so installer experience counts as much as the material. Plants that use epoxy resin flooring for industrial use in screed form should check this point first.
Check the Concrete Before Installing Chemical Resistant Flooring
Most failures of chemical resistant flooring start below the coating. Before any system goes down:
Concrete strength should be around M25 or higher for heavy-duty areas.
Test moisture. Rising damp causes blisters and peeling.
Shot blast or diamond grind the surface to open the pores.
Repair cracks and joints. Do not just cover them.
Remove oil contamination from the slab.
Skipping these steps is the most common reason a good product fails.
Practical Selection Checklist for Chemical Resistant Flooring
Match the system to the worst chemical on your list, not the average one.
Ask for a chemical resistance chart and check each chemical by name.
Compare cure time with your shutdown window.
Plan joints, drains and wall junctions, because leaks start there.
Ask about slip resistance in wet areas. A glossy floor can be risky.
Confirm which cleaners are safe and how often resealing may be needed.
Check that the epoxy flooring for industrial use you shortlist comes with a data sheet showing chemical and abrasion results.
Mistakes to Avoid
Buying chemical resistant flooring on price per square metre alone.
Ignoring thermal shock in washdown areas.
Using a standard epoxy where strong acids or solvents are present.
Skipping a test patch. A 1–2 square metre trial under real conditions for a week tells you more than any brochure.
Plan Before the Year-End Audit
Pharma, food and automotive plants usually schedule chemical resistant flooring work before audits. Surface testing, material supply and curing all take time, so a site assessment is best done now, not in the week before the shutdown. Early planning also lets you split the work area by area and keep production running.
Get Your Floor Assessed

Send your chemical list, area size and shutdown window, and the team at MB Enterprises will suggest a suitable chemical resistant flooring system. Use the "Request Site Assessment" button to book a visit.
FAQs
1. What is chemical resistant flooring made of?
Usually epoxy, novolac epoxy, polyurethane or vinyl ester resin mixed with fillers or aggregates. The right choice depends on the chemicals, temperature and traffic in your plant. A well-chosen industrial epoxy resin flooring system is the most common option.
2. Is epoxy safe for food plants?
A food safe epoxy system can be used in dry and moderately wet areas when it is low-odor and non-tainting. For hot, steam-cleaned zones, PU screed is often the better pick.
3. How thick should industrial screed flooring be?
Most systems fall between 4 and 9 mm. Heavy impact or hot spills call for the upper end.
4. How long does chemical resistant flooring last?
Many installations last 5 to 10 years or longer, depending on traffic, chemical exposure and maintenance. Poor surface preparation shortens this quickly.
5. How soon can chemical resistant flooring be used after installation?
Foot traffic is often possible within 24 hours, and vehicles after 2 to 3 days. Full chemical resistance usually needs about a week. Check the data sheet for your product and site temperature.
6. Can I apply new chemical resistant flooring over an old coating?
Only if the old coating is sound and well bonded. In most plants it is safer to remove it and prepare the concrete again.
Leave a Comment